

A swaging tool rarely fails all at once. It drifts. A roller develops a small flat, an axle picks up a little play, a shank loses some of its straightness, and the swaged lips coming off the machine start to look slightly different from the ones produced last quarter. By the time a proof load test fails, the tool may have been producing marginal results for weeks.
Bearing swaging tool inspection catches that drift early. This guide focuses on the wear indicators specific to swaging tools, especially tri-roller designs, and on how to turn them into a practical inspection routine. For broader guidance on tool care and calibration programs, see Bearing Tool Maintenance: How to Extend the Life of Your Aerospace Equipment and Aerospace Bearing Tool Calibration: Why Regular Inspection Matters.
Why Regular Swaging Tool Inspection Matters
A swaging tool transfers load to a lip that is only a fraction of a millimeter thick. Small changes in the tool’s contact surfaces translate into measurable changes in how that lip forms. The machine settings can stay identical while the result changes, because the tool itself is no longer the same.
Regular inspection protects three things. It protects the part, because a worn tool can crack a lip or damage a housing chamfer that cannot be reworked indefinitely. It protects the process, because consistent results depend on consistent tooling. And it protects your records, because an inspection history lets you separate tool-related problems from setup, material or operator issues when a defect appears.
Common Signs of Wear in Bearing Swaging Tools
Some wear is visible on the tool. Other wear shows up first on the parts. Both deserve attention, and the second category is often the earlier warning.
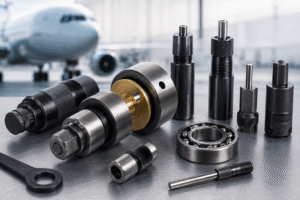
On the tool, look for scoring, pitting or flat spots on roller surfaces, material transferred from housings or bearings onto the rollers, rollers that turn roughly or bind, axial or radial play at roller axles, and visible bending or damage to the shank or pilot. On the parts, watch for lips that form unevenly around the circumference, new surface marks on the lip, a sudden rise in rotational torque after swaging, chamfer damage that did not appear before and an increase in proof load failures or borderline results.
| Wear indicator | Where it appears | What it can mean |
|---|---|---|
| Flat spots or pitting on rollers | Roller contact surface | Uneven contact, marks on the lip |
| Material pickup | Roller surface | Galling, poor surface finish on the swage |
| Rough or tight roller rotation | Roller and axle | Worn axle, contamination, damaged roller bearing |
| Play at the roller axle | Roller mount | Rollers shift under load, inconsistent lip formation |
| Shank runout | Tool body and shank | Misalignment, one-sided swaging |
| Uneven lip formation on parts | Swaged bearing | Any of the above, or setup and fixturing issues |
Inspecting Rollers, Contact Surfaces, and Tool Components
Clean the tool before inspecting it. Residue from lubricants and transferred metal hides surface defects and can make a roller feel smoother or rougher than it is. Use the cleaning method approved in your shop and the tool documentation.
Rollers and contact surfaces
Examine each roller under good light and magnification. The contact zone should be smooth and continuous, with no flats, chips, pits or embedded material. Rotate each roller by hand. It should turn freely and evenly with no catching. Compare the three rollers of a tri-roller tool against each other, because one roller wearing faster than the others is a classic source of one-sided swaging.
Profile matters as much as finish. Tri-roller swaging tools are matched to bearing lip geometry, and wear that changes the roller profile changes how the lip forms even when the surface still looks clean. If your quality system provides profile gauges or reference parts, use them here.
Axles, mounts and tool body
Check each roller axle for play by applying light pressure in the axial and radial directions. Any movement beyond what the tool documentation allows means the roller can shift under load. Inspect the roller mounts and tool body for cracks, deformation and loose fasteners.
For drill press tools, check shank straightness and runout in a suitable fixture, because a bent shank produces off-center swaging no matter how good the rollers are. For portable tools, inspect handles, guides and any alignment features that keep the tool square to the bearing during operation.
How Tool Wear Can Affect Swaging Consistency
Wear changes the contact between tool and lip. A flat spot concentrates load at one point in each revolution. Axle play lets a roller drift away from the lip under load. Runout tilts the entire contact pattern. Each mechanism leaves the operator’s settings unchanged while the deformation of the lip changes.
The effects compound. A slightly worn tool may still produce acceptable parts, so the wear goes unnoticed. Operators compensate by adjusting pressure or adding revolutions. That compensation raises the load on already worn rollers and accelerates the wear further. Inspection breaks this cycle by tying a change in results back to the tool before it becomes a pattern. The article Bearing Swaging Quality Control explains how tool condition fits into a wider quality program.
Creating a Swaging Tool Inspection Checklist
A checklist makes inspection repeatable across shifts and inspectors. Keep it short enough to use and specific enough to catch real problems. The template below covers the main points. Adjust it to your tools and to the inspection frequency your quality system defines.
| Item | Check | Accept / Reject / Notes |
|---|---|---|
| Tool identification | Tool ID, bearing part numbers covered, last inspection date | |
| Cleanliness | No residue or transferred material | |
| Roller surfaces | No flats, pits, scoring or chips | |
| Roller rotation | Free, smooth, even across all rollers | |
| Axle play | Within the limits in the tool documentation | |
| Roller profile | Matches gauge or reference part, if available | |
| Shank or guide | Straight, no damage, runout within limits | |
| Body and fasteners | No cracks, deformation or loose fasteners | |
| Trial swage | Result on a test part or first part meets procedure criteria | |
| Records | Findings, actions and inspector signature logged |
Base the inspection frequency on usage, results and your quality procedures. A tool used every shift on high-volume work needs closer attention than one used occasionally in MRO. Add an inspection trigger after any abnormal event: a dropped tool, a failed proof load test or a visible change in swaged parts.
When Should Swaging Equipment Be Serviced or Replaced?
Service the tool when inspection finds wear that can be corrected, such as a roller or axle that can be replaced according to the manufacturer’s guidance. Remove the tool from use when a defect affects contact geometry or alignment and cannot be restored, or when results no longer meet the procedure’s acceptance criteria after correction.
Do not rework rollers or modify tool geometry on your own. The tool’s profile is matched to the bearing, and an unapproved change can create defects that look like operator or material problems. Contact the tool manufacturer for service, replacement components or a replacement tool. Aero Staking supplies both Portable Tri-Roller Swaging Tools and the Drill Press Tri-Roller Swaging Tool line.
Frequently Asked Questions
How often should bearing swaging tools be inspected?
There is no single interval for every shop. Set the frequency through your quality system based on usage, criticality and results, and add inspections after abnormal events such as a drop or a failed test.
What is the first sign of swaging tool wear?
Often it appears on the parts before it is obvious on the tool: uneven lip formation, new marks on the swage, higher rotational torque or borderline proof load results.
Can I polish a worn roller to restore it?
Avoid modifying rollers unless the tool manufacturer provides an approved procedure. Polishing can change the profile that forms the lip.
Does swaging tool wear affect proof load results?
It can. Wear that reduces or unevenly distributes contact leaves parts of the lip under-formed, which lowers retention. Testing Tools help confirm that the swage meets the required load.
Is tool inspection the same as calibration?
No. Inspection checks the physical condition of the tool. Calibration verifies measuring equipment against a reference. Both belong in a complete aerospace tool maintenance program.
Conclusion: Maintaining Reliable Swaging Operations
The most useful inspection data does not come from the tool alone. It comes from comparing what the tool looks like with what the parts look like over time. A shop that logs both can see wear developing long before it becomes a rejected part, and can plan service instead of reacting to a failure.
Build that connection into your routine: inspect rollers, axles and alignment, record the condition, and link it to the swaged parts and test results that follow. When a tool reaches the end of its service life, replace it with tooling matched to your bearing part numbers. Review Aero Staking’s swaging tools or contact Aero Staking for service and replacement options.